IBC Bin Manufacturer
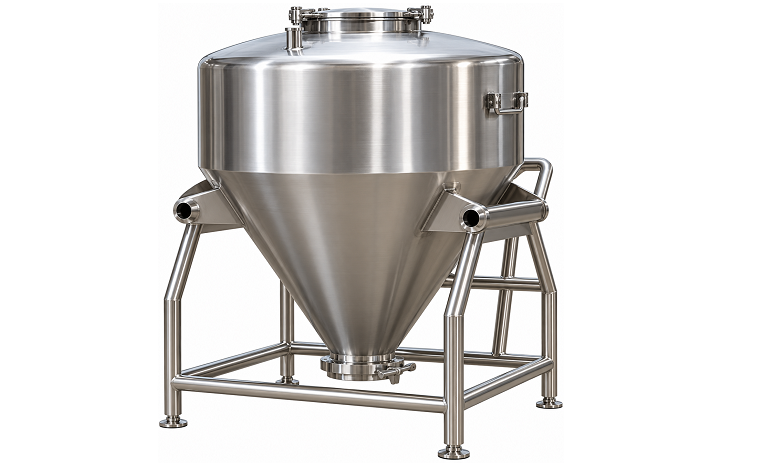
Equilateral Solutions manufactures high-quality Pharmaceutical IBC Bins (Intermediate Bulk Containers) designed for hygienic storage, handling, transfer, and controlled discharge of pharmaceutical powders, granules, excipients, and intermediate products.
Our pharmaceutical IBC bins are engineered to support efficient material handling between different stages of pharmaceutical manufacturing while maintaining product integrity and minimizing contamination risks. Manufactured using premium-grade SS304, SS316, or SS316L stainless steel, these containers feature GMP-oriented hygienic construction, smooth product-contact surfaces, hygienically finished welds, and easy-to-clean designs.
Designed for compatibility with modern pharmaceutical production facilities, our IBC bins provide convenient material transfer, controlled powder discharge, and efficient integration with blending, granulation, milling, tablet compression, and capsule filling operations.
Available in capacities ranging from 100 litres to 1,000 litres, our pharmaceutical IBC bins can be customized according to batch size, bulk density, powder flow characteristics, material handling requirements, and customer User Requirement Specifications (URS).
Key Features of Pharmaceutical IBC Bins
1. GMP & Hygienic Design
Our pharmaceutical IBC bins are designed around GMP and hygienic engineering principles to support safe material handling and effective cleaning.
Key design features include:
- – Smooth internal product-contact surfaces.
- – Hygienically finished internal welds.
- – Minimized product retention areas.
- – Dust-tight construction.
- – Suitable sanitary connections.
- – Easy-to-clean internal geometry.
- – Accessible inspection and maintenance arrangements.
The design can be customized according to pharmaceutical manufacturing and cleaning requirements.
2. SS304 / SS316 / SS316L Stainless Steel Construction
Our IBC bins are manufactured using high-quality stainless steel selected according to product characteristics and process requirements.
- – SS304: Suitable for compatible pharmaceutical powders, excipients, and general hygienic material handling applications.
- – SS316: Provides enhanced corrosion resistance for demanding pharmaceutical applications.
- – SS316L: Suitable for pharmaceutical product-contact applications requiring low-carbon stainless steel construction and enhanced corrosion resistance.
Product-contact surfaces can be polished to Ra ≤ 0.8 µm or better, as specified in the project URS.
3. Optimized Powder Discharge System
The IBC bins feature customized sloped or pyramidal bottom configurations to facilitate controlled discharge of powders and granules.
The bottom geometry, outlet dimensions, and discharge mechanism are selected according to material flow properties, bulk density, particle size, and batch requirements.
Available discharge arrangements include:
- – Hygienic butterfly valves.
- – Pneumatic-operated discharge valves.
- – Customized outlet connections.
- – Dust-tight discharge arrangements.
- – Adaptable connections for downstream processing equipment.
4. Easy Material Handling & Mobility
Our pharmaceutical IBC bins are designed for convenient movement and handling within manufacturing facilities.
Depending on the configuration, they can be handled using:
- – Forklifts.
- – Pallet trucks.
- – Dedicated lifting systems.
- – Optional castor-wheel arrangements.
- – Customized material handling equipment.
The supporting frame and lifting arrangements can be engineered according to the required working load and handling method.
5. Customized Design & Configuration
IBC bins can be customized according to batch size, production requirements, plant layout, and material characteristics.
Customization options include:
- – Customized tank dimensions and capacity.
- – Sloped or pyramidal bottom geometry.
- – Customized outlet size and arrangement.
- – Top charging openings and covers.
- – Supporting frame configurations.
- – Lifting and handling arrangements.
- – Castor wheels, where required.
- – Customized internal surface finish.
- – Dust-tight covers and connections.
6. Dust-Tight & Contamination-Controlled Construction
Pharmaceutical powder handling requires suitable protection against external contamination and uncontrolled dust release.
Our IBC bins can incorporate sealed covers, suitable gaskets, dust-tight connections, and enclosed discharge arrangements to support controlled powder transfer and handling.
7. Integration with Pharmaceutical Process Equipment
Our pharmaceutical IBC bins can be integrated with different processing and material handling systems to support efficient manufacturing workflows.
Compatible equipment includes:
- – IBC blenders and bin blenders.
- – Vibro sifters.
- – Multimills and pulverizers.
- – Vacuum transfer systems.
- – Powder conveying systems.
- – Tablet compression machines.
- – Capsule filling machines.
- – Granulation and blending equipment.
Applications of Pharmaceutical IBC Bins
Our pharmaceutical IBC bins are suitable for hygienic storage, handling, and transfer of a wide range of pharmaceutical raw materials and intermediate products.
- – Active Pharmaceutical Ingredients (APIs): Handling and transfer of compatible active pharmaceutical ingredients.
- – Pharmaceutical Excipients: Storage and transfer of lactose, microcrystalline cellulose, starch, and other formulation excipients.
- – Tablet Manufacturing: Handling of blended powders and granules used in tablet production.
- – Capsule Manufacturing: Transfer and storage of powder formulations used in capsule filling.
- – Granules: Handling of wet or dry granules, depending on material characteristics and container configuration.
- – Nutraceutical Products: Storage and transfer of protein powders, vitamins, minerals, and nutritional ingredients.
- – Dry Powder Formulations: Handling of pharmaceutical dry blends and intermediate formulations.
- – Premixes: Storage and transfer of prepared pharmaceutical and nutraceutical premixes.
Technical Specifications of Pharmaceutical IBC Bins
| Parameter | Specification |
|---|---|
| Equipment Type | Pharmaceutical IBC Bin |
| Capacity | 100 L to 1,000 L |
| Material of Construction | SS304 / SS316 / SS316L |
| Design | GMP-Oriented Hygienic Design |
| Configuration | Mobile / Customized |
| Bottom Design | Sloped / Pyramidal / Customized |
| Internal Surface Finish | Ra ≤ 0.8 µm or as per URS |
| Welding | Hygienically Finished |
| Discharge Arrangement | Hygienic Butterfly Valve / Customized |
| Charging Arrangement | Top Opening / Covered Inlet |
| Handling System | Forklift / Pallet Truck / Lifting System |
| Mobility | Optional Castor Wheels |
| Surface Finish | Internal / External Polishing as Required |
| Sealing | Suitable Food / Pharmaceutical-Grade Gaskets |
| Dust Protection | Dust-Tight Cover and Connections |
| Integration | IBC Blender / Sifter / Mill / Powder Transfer System |
| Design & Capacity | Fully Customizable |
Note: Final IBC dimensions, material thickness, surface finish, outlet configuration, frame design, and accessories are selected according to customer URS, batch size, bulk density, and material flow characteristics.
Available Pharmaceutical IBC Bin Capacities
Equilateral Solutions offers pharmaceutical IBC bins in different capacities to support small, medium, and large-scale manufacturing operations.
100 L | 150 L | 200 L | 300 L | 400 L | 500 L | 600 L | 750 L | 800 L | 1,000 L
Customized capacities and configurations are also available according to batch requirements, powder characteristics, bulk density, handling equipment, and production workflows.
Advantages of Pharmaceutical IBC Bins
- – Hygienic Material Handling: Stainless steel construction supports hygienic storage and transfer of pharmaceutical ingredients.
- – Reduced Contamination Risks: Dust-tight covers and suitable sealing arrangements help protect materials during handling.
- – Efficient Material Transfer: Designed for convenient movement between different pharmaceutical processing stages.
- – Controlled Powder Discharge: Customized bottom geometry and discharge valves support controlled material transfer.
- – Reduced Product Retention: Smooth internal surfaces and optimized geometry help minimize material hold-up.
- – Easy Cleaning: Accessible construction and suitable internal surface finishes facilitate cleaning.
- – Improved Production Efficiency: Reduces manual material handling and supports organized manufacturing workflows.
- – Equipment Integration: Compatible with IBC blenders, sifters, mills, tablet presses, and capsule filling systems.
Customized Pharmaceutical IBC Bin Solutions
Equilateral Solutions provides customized Pharmaceutical Stainless Steel IBC Bins engineered according to specific material handling, storage, and production requirements.
From compact batch containers to large-capacity intermediate bulk containers, our solutions can be configured with suitable stainless steel grades, capacities, bottom geometry, discharge valves, supporting structures, lifting arrangements, surface finishes, and dust-tight connections.
Our focus on hygienic fabrication, material quality, operational flexibility, and application-specific engineering helps pharmaceutical manufacturers improve powder handling, minimize material loss, and streamline production workflows.
Why Choose Equilateral Solutions for Pharmaceutical IBC Bins?
Equilateral Solutions specializes in manufacturing stainless steel process equipment and hygienic material handling solutions for pharmaceutical and allied industries.
Our pharmaceutical IBC bins are engineered with a focus on GMP-oriented construction, reliable powder discharge, easy material handling, and integration with existing pharmaceutical production equipment.
We develop customized solutions according to customer URS, batch requirements, material properties, and plant layout.
Enquire About Pharmaceutical IBC Bins
Looking for a customized Pharmaceutical IBC Bin for your manufacturing facility?
Contact Equilateral Solutions to discuss your requirements for SS316L pharmaceutical IBC bins, intermediate bulk containers, and hygienic powder handling equipment.