Stainless Steel Reactor for Pharmaceutical Industry
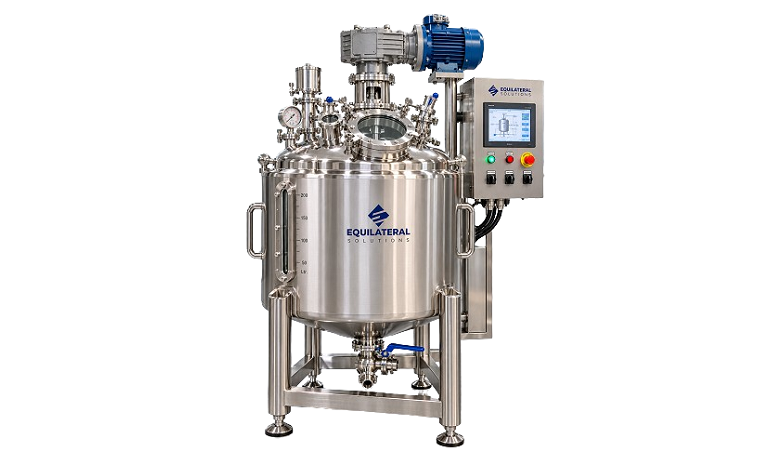
Equilateral Solutions manufactures high-quality Stainless Steel Reactors for pharmaceutical applications involving mixing, heating, cooling, dissolution, reaction, and product preparation.
Our pharmaceutical reactors are manufactured using SS304 or SS316L stainless steel, with hygienic design features suitable for pharmaceutical processing. They can be supplied with heating and cooling jackets, agitators, sanitary fittings, instrumentation, insulation, and CIP provisions according to specific process requirements.
Available in capacities ranging from 100 litres to 2,000 litres, our stainless steel reactors can also be customized in terms of capacity, configuration, operating conditions, and process connections to suit different pharmaceutical manufacturing applications.
Key Features of Stainless Steel Reactors
1. Hygienic & GMP-Oriented Design
Designed for pharmaceutical processing environments, our reactors feature smooth internal surfaces, sanitary connections, hygienic construction, and easy-cleaning provisions. The design can be configured to support the applicable process and cleaning requirements.
2. SS304 / SS316L Stainless Steel Construction
Our reactors are available in SS304 and SS316L stainless steel. Material selection is based on product compatibility, corrosion resistance, process conditions, and customer requirements.
3. Heating & Cooling Arrangement
Reactors can be supplied with heating and cooling jackets to support controlled processing temperatures. Optional thermal insulation, temperature sensors, and monitoring provisions can also be incorporated according to the application.
4. Customized Agitation System
Our pharmaceutical reactors are available with top-mounted geared agitators and VFD-controlled drives. The agitator configuration can be customized according to product viscosity, batch volume, and mixing requirements.
5. CIP & Sanitary Connections
The reactors can be provided with CIP spray balls, sanitary inlet and outlet connections, customized nozzles, instrumentation ports, and hygienic valves to support efficient operation and cleaning.
6. Customized Process Design
Depending on process requirements, reactors can be designed for atmospheric, pressure, or vacuum operation. Skid-mounted systems and customized nozzle orientations can also be provided according to the installation layout and process specifications.
Applications of Stainless Steel Reactors in Pharmaceutical Industry
Our stainless steel reactors are suitable for a wide range of pharmaceutical, nutraceutical, and allied manufacturing applications, including:
- – Liquid Formulation: Preparation and processing of pharmaceutical liquid formulations.
- – Syrup Preparation: Mixing and dissolution of ingredients for pharmaceutical syrups.
- – Solution Preparation: Preparation and blending of pharmaceutical solutions.
- – Ingredient Dissolution: Dissolving compatible raw materials and ingredients under controlled processing conditions.
- – Pharmaceutical Reactions: Carrying out process-specific reactions in suitable reactor configurations.
- – Mixing & Blending: Uniform mixing of liquid and compatible semi-liquid ingredients.
- – Buffer Preparation: Preparation and mixing of buffer solutions for pharmaceutical processes.
- – API Processing: Suitable process applications involving active pharmaceutical ingredients, subject to material compatibility and process requirements.
- – Ointment & Cream Manufacturing: Preparation and processing of compatible semi-solid formulations.
- – Nutraceutical Applications: Mixing and preparation of liquid formulations and nutritional products.
Technical Specifications of Stainless Steel Reactor
| Parameter | Specification |
|---|---|
| Equipment Type | Stainless Steel Reactor |
| Application | Pharmaceutical / Nutraceutical Processing |
| Capacity | 100 L to 2,000 L |
| Material of Construction | SS304 / SS316L |
| Design | Hygienic / GMP-Oriented |
| Operating Configuration | Atmospheric / Pressure / Vacuum, as specified |
| Agitator Arrangement | Top-Mounted / Customized |
| Agitator Drive | Geared Motor with VFD Control |
| Heating / Cooling | Jacketed Arrangement – Optional |
| Insulation | Optional |
| Temperature Monitoring | Temperature Sensor / RTD |
| CIP Arrangement | CIP Spray Ball – Optional |
| Connections | Sanitary Fittings / Customized Nozzles |
| Instrumentation | As per Process Requirements |
| Installation | Floor-Mounted / Skid-Mounted |
| Design & Configuration | Fully Customizable |
Note: Final capacity, material grade, wall thickness, agitator configuration, motor rating, jacket arrangement, operating pressure, vacuum requirements, and instrumentation are selected according to the process requirements and customer specifications.
Standard Reactor Capacities
Equilateral Solutions manufactures stainless steel reactors in capacities ranging from 100 litres to 2,000 litres, with customized configurations available to suit different pharmaceutical production requirements.
Custom capacities, operating conditions, agitator arrangements, heating and cooling systems, and instrumentation can be engineered according to the intended process and plant layout.
Advantages of Stainless Steel Reactors
- – Hygienic Processing: Stainless steel construction and suitable surface finishes support pharmaceutical processing requirements.
- – Corrosion Resistance: SS304 and SS316L material options provide corrosion resistance in suitable operating environments.
- – Controlled Processing: Optional heating and cooling arrangements support temperature-controlled operations.
- – Efficient Mixing: Application-specific agitator designs support uniform mixing and blending.
- – Easy Cleaning: CIP provisions and sanitary connections facilitate cleaning operations.
- – Flexible Configuration: Atmospheric, pressure, and vacuum configurations can be selected according to process requirements.
- – Process Integration: Customized nozzles, fittings, and skid-mounted arrangements support integration with existing production systems.
- – Application-Specific Design: Capacities, accessories, and instrumentation can be tailored to individual manufacturing needs.
Customized Pharmaceutical Reactor Solutions
Equilateral Solutions manufactures customized stainless steel pharmaceutical reactors designed to meet the specific requirements of pharmaceutical and nutraceutical manufacturing facilities.
From liquid formulation and syrup preparation to solution processing, ingredient dissolution, and pharmaceutical reactions, our reactors can be configured with suitable stainless steel grades, capacities, agitation systems, heating and cooling jackets, insulation, sanitary connections, CIP provisions, and instrumentation.
Our focus on hygienic engineering, quality fabrication, process-specific design, and customization helps manufacturers select reactor systems suited to their production processes and operational requirements.
Get a Quote for Stainless Steel Pharmaceutical Reactors
Looking for a customized Stainless Steel Reactor for your pharmaceutical manufacturing facility? Contact Equilateral Solutions to discuss your requirements for hygienic pharmaceutical reactors and stainless steel process equipment.